
Leave Your Message
Purpose-built water storage systems designed to meet the massive daily water demands of mega retail environments — from fire suppression reserves to potable water supply.
As global urbanization accelerates and mega shopping malls expand in scale and complexity, reliable water storage and management infrastructure has become a mission-critical investment.
The global commercial water tank market is projected to surpass USD 4.2 billion by 2030, driven by rapid construction of large-scale retail complexes across Asia-Pacific, the Middle East, and Southeast Asia. Countries like China, Indonesia, Vietnam, and Thailand are witnessing an unprecedented surge in new mall developments, each requiring sophisticated multi-zone water storage solutions.
Modern mega malls are no longer simple retail spaces — they are integrated lifestyle hubs combining hotels, offices, entertainment zones, and residential towers. This multi-functional complexity demands water tanks that can serve diverse pressure zones, maintain hygienic standards across potable and non-potable circuits, and integrate seamlessly with BMS (Building Management Systems).
With LEED, BREEAM, and local green building certifications becoming mandatory for large commercial projects, developers are increasingly specifying enamel-coated steel tanks for their superior hygiene performance, reduced maintenance footprint, and compatibility with rainwater harvesting and greywater recycling systems — key contributors to sustainability scoring.
Regulatory frameworks across global markets — including NFPA, EN 12845, and GB50016 — mandate dedicated fire reserve water storage in commercial facilities. Enamel steel tanks, with their high structural integrity and certified corrosion resistance, are increasingly the preferred choice for compliant fire suppression water storage in large-footprint commercial developments.
Engineered for the unique operational demands of high-traffic commercial facilities, enamel steel tanks offer an unmatched combination of hygiene, durability, and design flexibility.
High-temperature sintered enamel coating forms a chemically inert glass-like barrier on the steel substrate, providing exceptional resistance to corrosion, bacteria, and chemical attack — essential in humid mall mechanical rooms.
Non-toxic, smooth enamel interior surface meets NSF/ANSI 61, GB/T 17393, and international drinking water standards — critical for malls serving thousands of daily visitors through restaurants, cafes, and public amenities.
Bolt-assembled panel construction enables flexible volume configurations from 1 m³ to 10,000+ m³, allowing phased expansion as mall footfall grows — without structural demolition or operational downtime.
Compatible with IoT water level sensors, automated pressure management, and BMS integration for real-time monitoring of water quality, storage levels, and pump performance across multiple tank zones within a mall complex.
Premium steel substrate with reinforced panel joints ensures structural integrity under seismic loads, thermal expansion, and the high static pressures required by multi-story mall water distribution systems.
Enamel-coated steel tanks typically achieve 30+ year service life with minimal maintenance — delivering exceptional lifecycle cost performance compared to GRP or concrete alternatives in demanding commercial environments.
From rooftop gravity tanks to underground fire reserves, enamel steel water tanks serve multiple critical functions across the full infrastructure spectrum of modern commercial complexes.
Mega malls are required by law to maintain dedicated fire water reserves — typically 200–1,000+ m³ depending on floor area. Enamel steel tanks, with their certified pressure resistance and corrosion-proof interiors, provide code-compliant fire reserve storage that remains reliable over decades without degradation of water quality or structural integrity. Underground installation options maximize usable retail floor space while meeting all fire authority requirements.
Public restrooms, food court kitchens, specialty restaurants, supermarkets, and hotel components within mixed-use malls require safe, hygienic potable water storage. The glass-smooth enamel surface prevents bacterial biofilm formation and algae growth, ensuring water quality compliance with WHO and local health authority standards — protecting both mall visitors and operators from liability.
Large-scale HVAC systems serving multi-zone mall environments consume significant makeup water for cooling towers and chiller systems. Enamel steel tanks serve as buffer storage for treated cooling water, preventing system downtime during peak demand periods and ensuring consistent thermal management across anchor stores, food courts, and entertainment zones with varying heat loads.
Green-certified mall developments increasingly deploy enamel steel tanks as collection and treatment buffer vessels for greywater recycling (toilet flushing, irrigation) and rainwater harvesting systems. The inert enamel coating is compatible with treated greywater chemistry, while the modular design allows dedicated segregated storage circuits — supporting LEED credits for water efficiency and reduced municipal water consumption.
Premium malls incorporating water parks, indoor pools, decorative fountains, and spa facilities require high-capacity, hygienic buffer storage for treated recreational water. Enamel steel tanks provide the corrosion resistance needed for chlorinated and chemically treated water systems, while their smooth interior surfaces simplify cleaning and maintenance — critical for facilities with strict public health inspection regimes.
The modular bolt-assembled construction of enamel steel tanks makes them ideal for temporary water supply during mall construction phases — easily relocated and repurposed as permanent infrastructure upon project completion. This flexibility delivers significant cost savings for mall developers managing complex, multi-phase construction programs across large sites.
Shandong Fengdun Environmental Technology Co., Ltd. is located in Luquantun Industrial Development Zone, Dezhou City. It is adjacent to the Beijing-Kowloon artery to the east, the provincial capital Jinan to the south, and the Beijing-Hangzhou Canal to the north, with convenient transportation and fast communication.
The company has a strong professional R&D team, and "Feng Shield" has also become a well-known brand in the ventilation equipment manufacturing industry. As an original manufacturer of HVAC, ventilation equipment, water tanks, and cooling towers, we offer factory-direct pricing with zero middleman markup — delivering the most competitive solutions to global clients.
VIEW MORE
Global project solutions for commercial water infrastructure, industrial cooling, and environmental systems — delivered by Fengdun's expert engineering team.
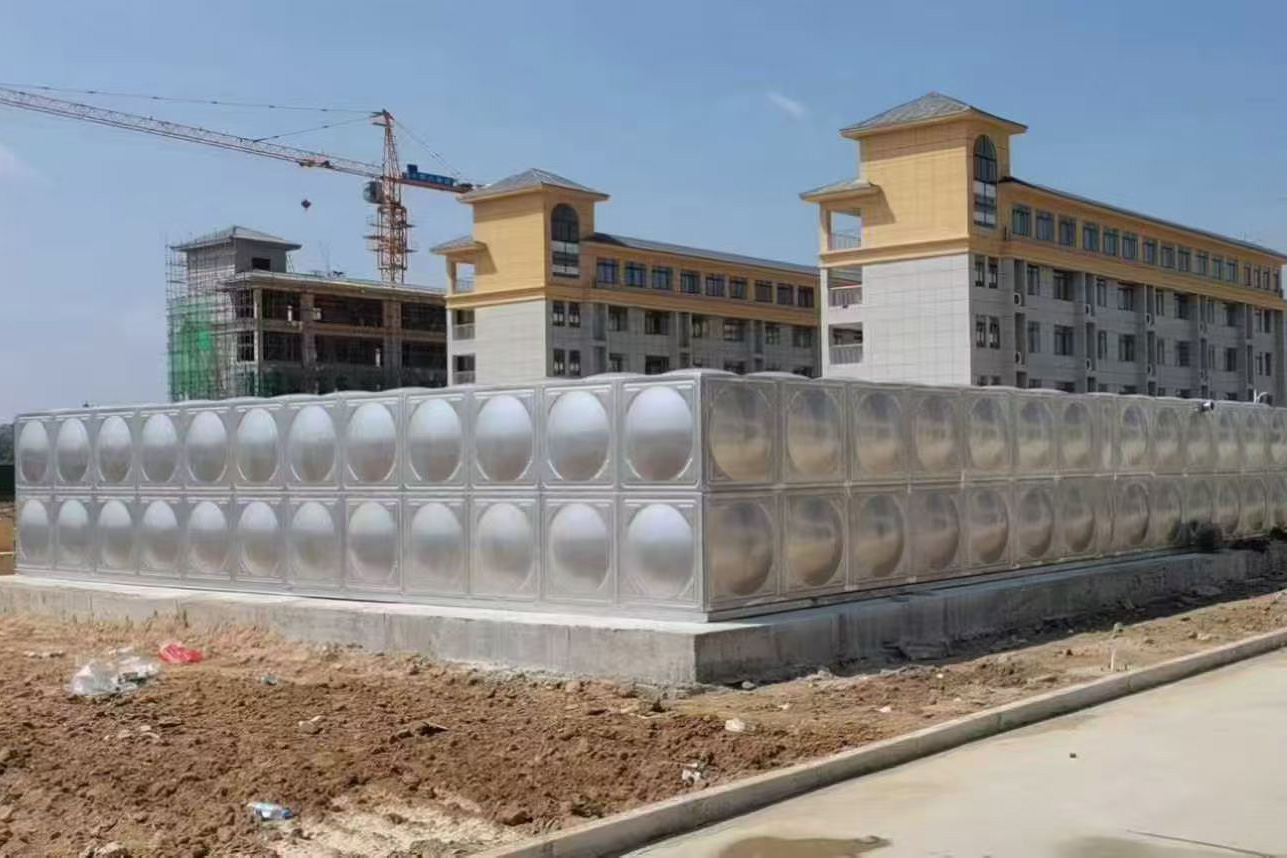
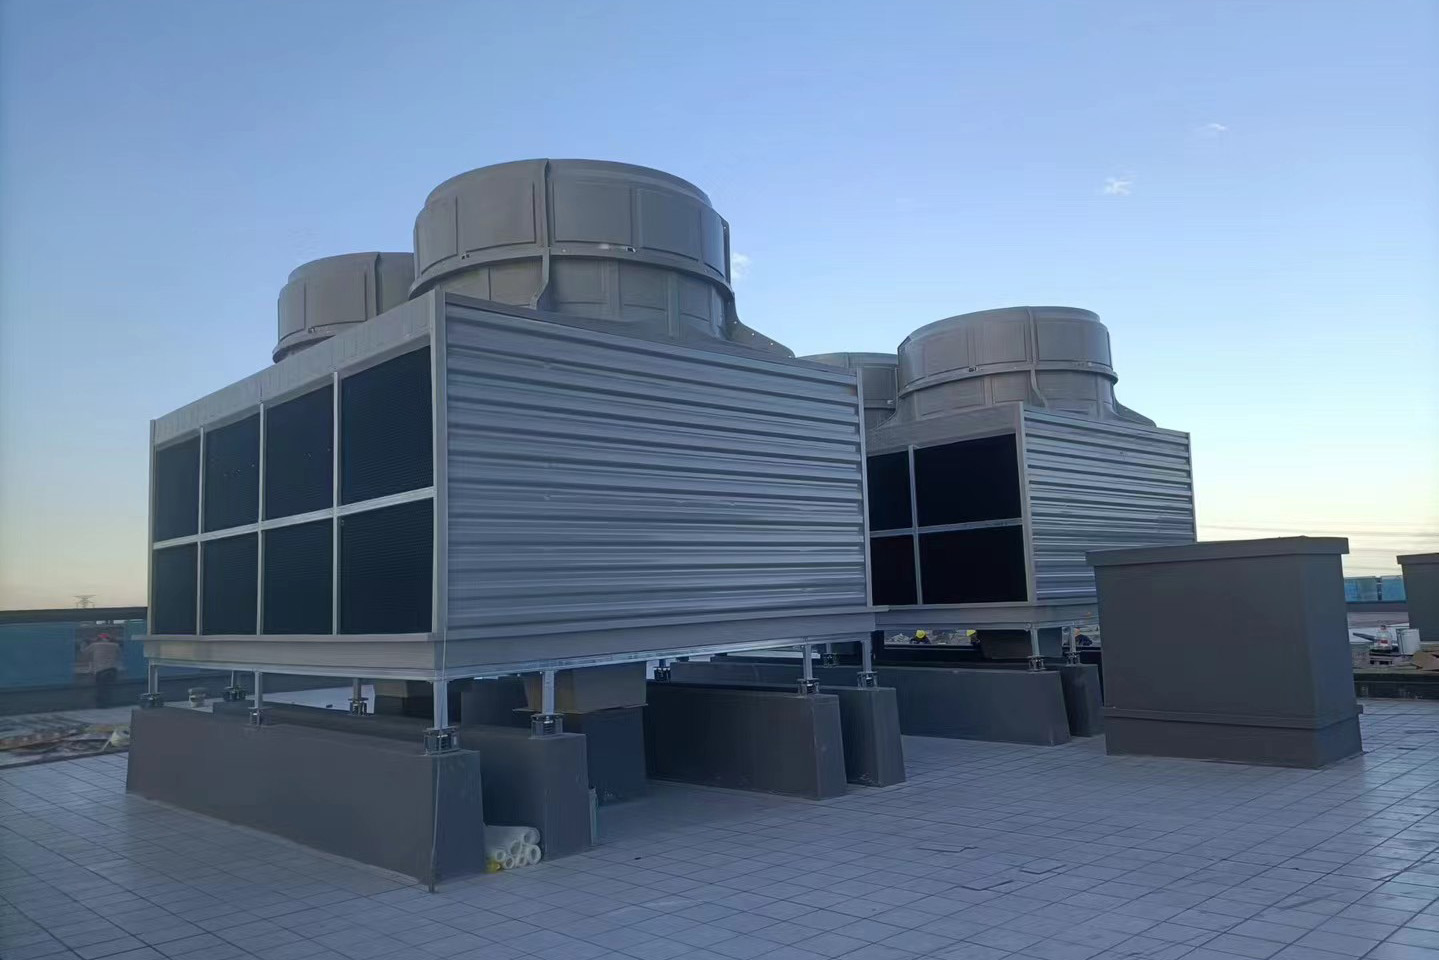
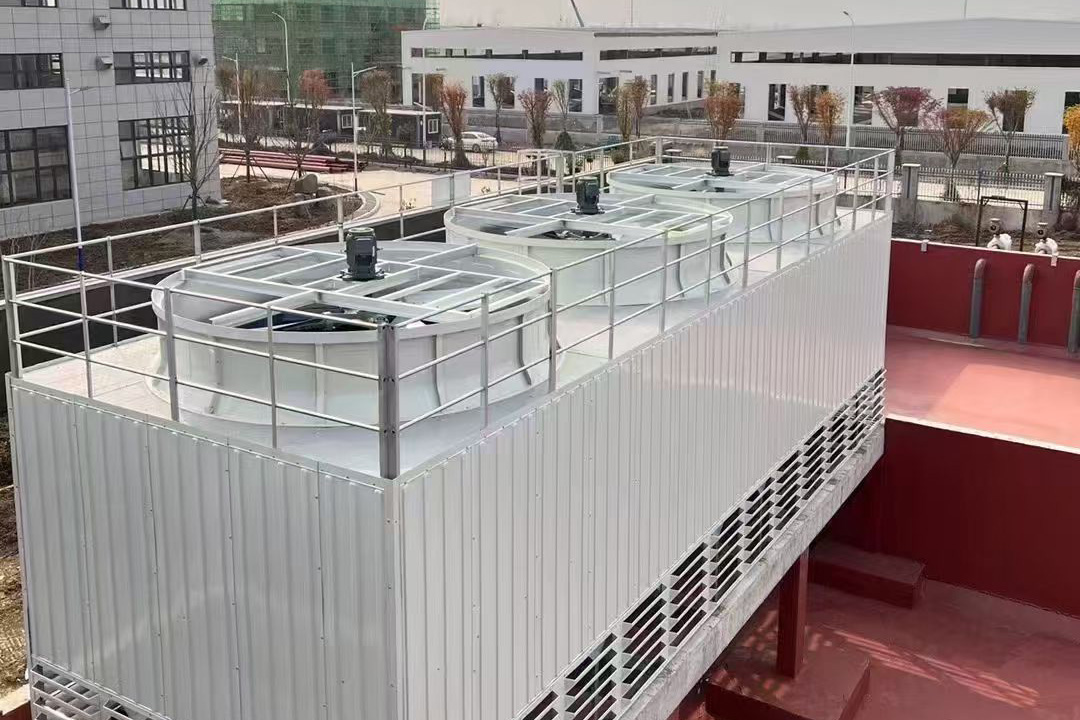
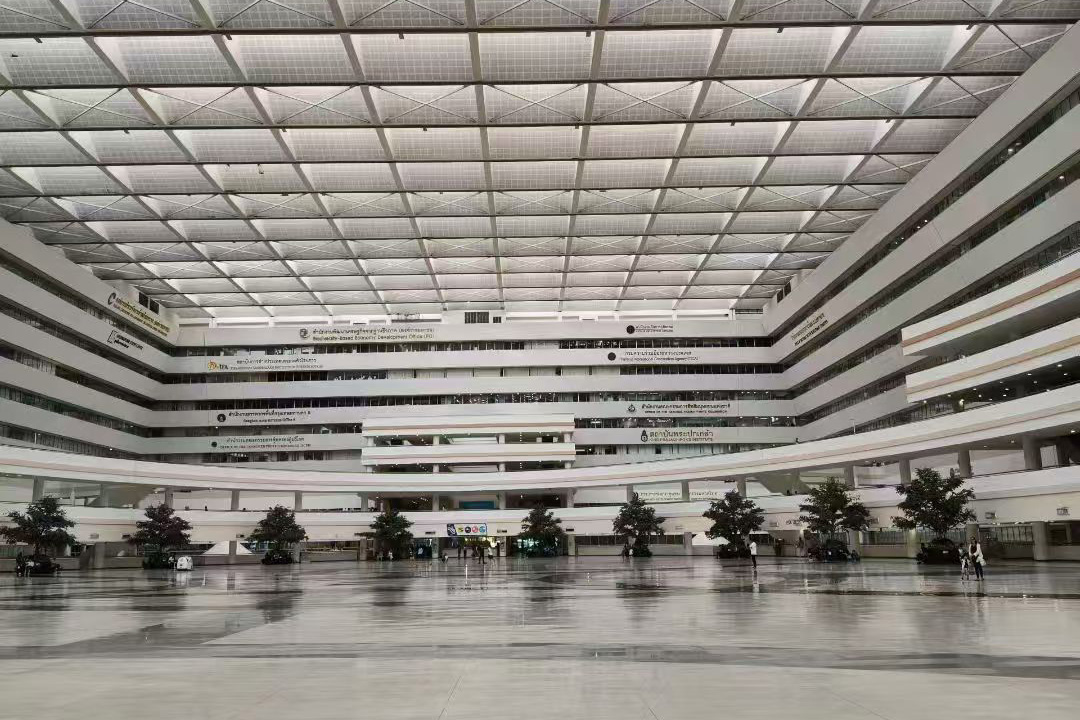
Fengdun Environmental Technology is an original manufacturer of HVAC and ventilation equipment. We independently produce a full range of products including fans, air dampers, water tanks and cooling towers. With no middleman markup, we offer overseas clients the most competitive factory-direct prices.
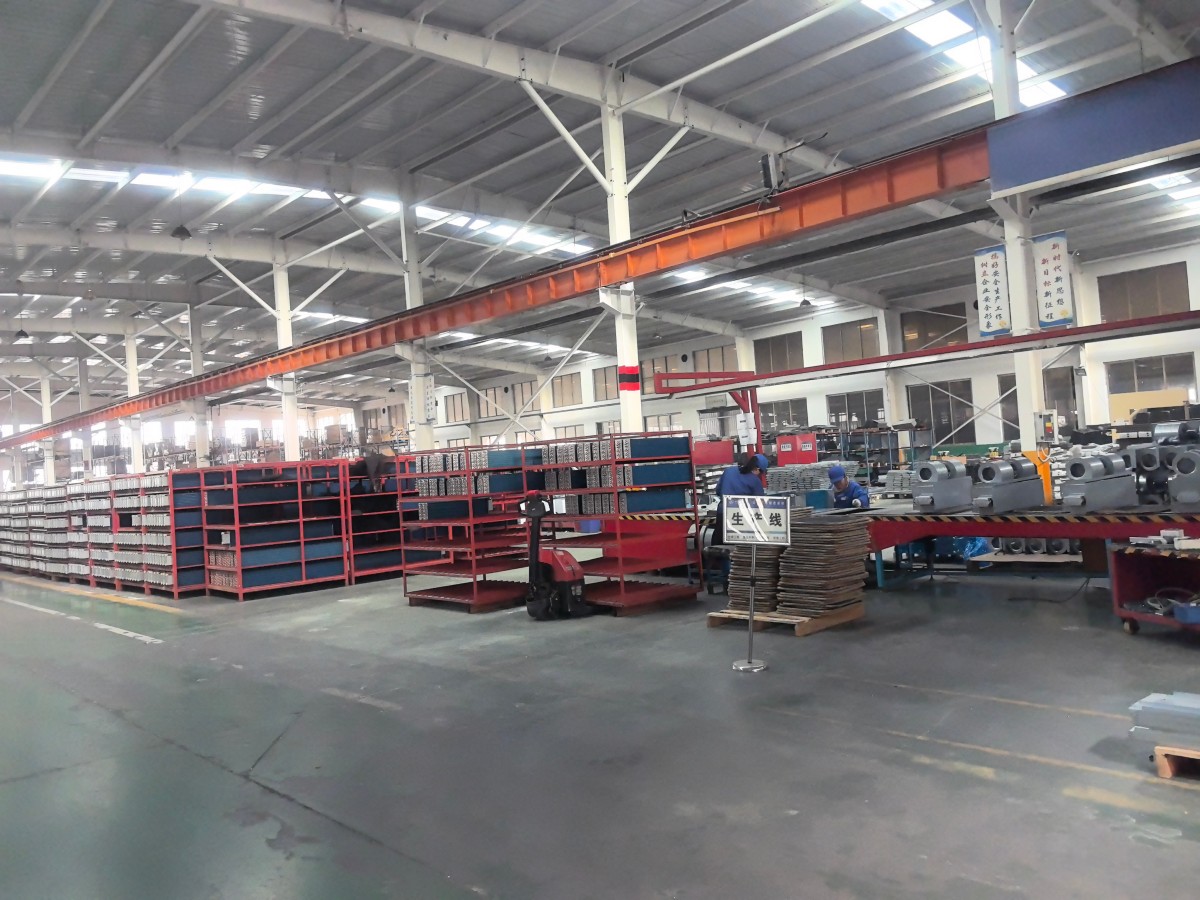
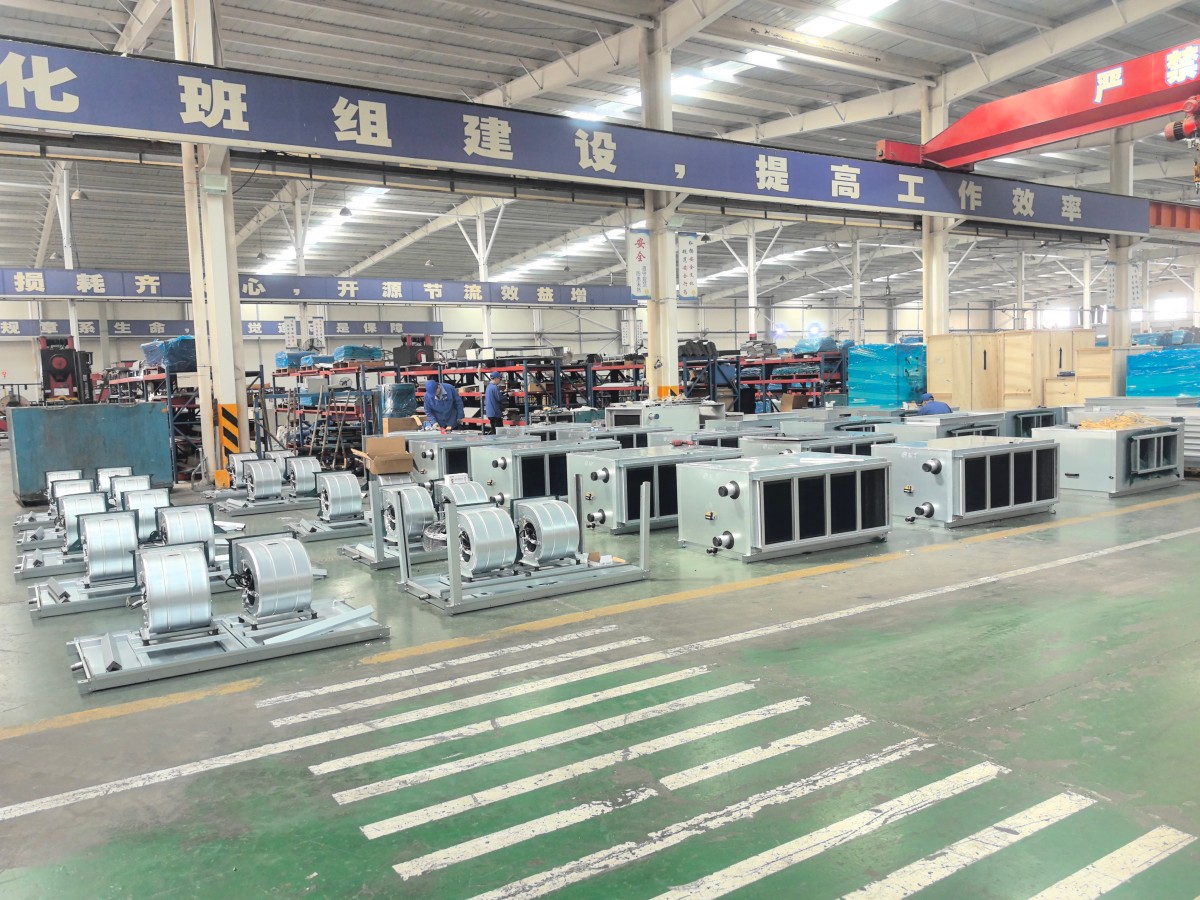
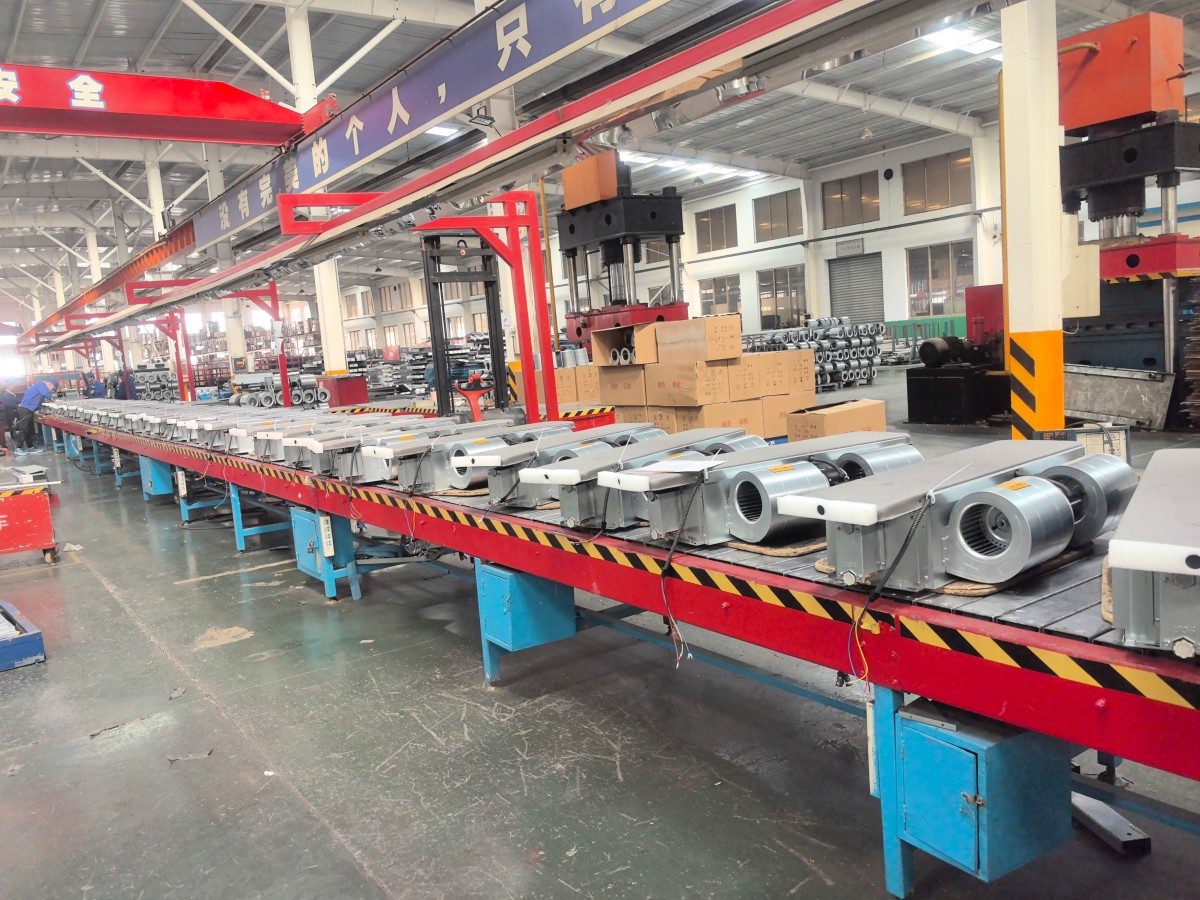
The company adheres to the principles of "development and production simultaneously" and "sales and service simultaneously". Meeting customer requirements is our eternal pursuit of business principles, and we advocate the concept of quality over price.
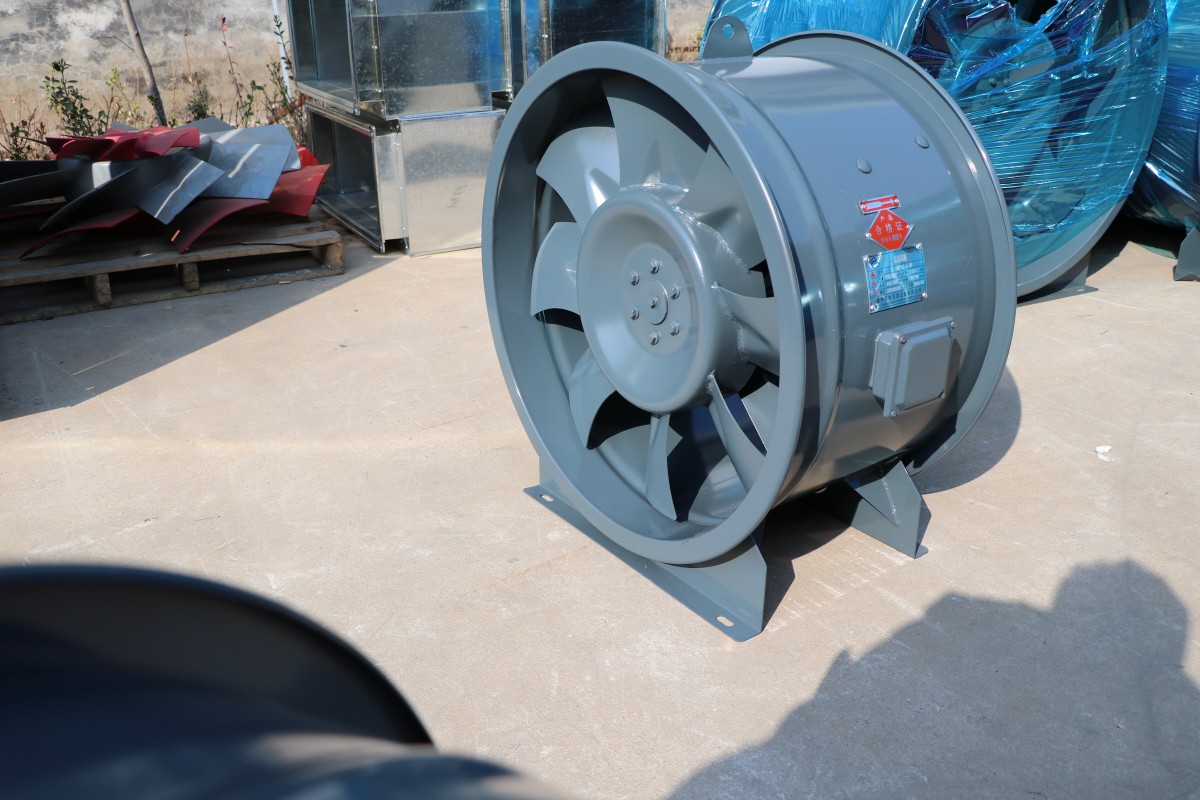
Explore our complete range of water tanks, cooling towers, fans, and ventilation solutions — all manufactured to international standards and available for global export.
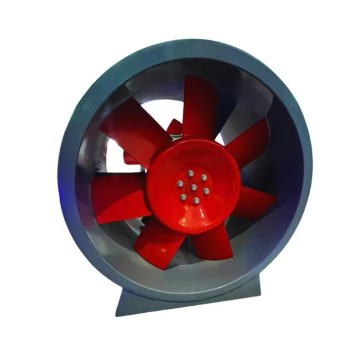
High temperature resistance, low noise, stable operation and high efficiency. Durable, energy-saving, with large air volume and reliable performance for long-term use.
MORE PRODUCTS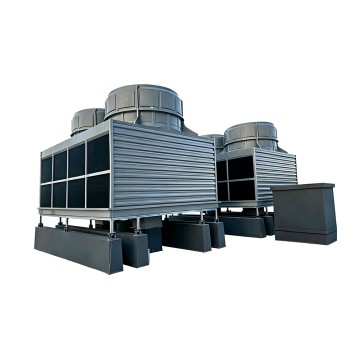
Efficient heat dissipation for industrial and HVAC systems. Available in durable FRP or sturdy galvanized steel construction to suit different working environments.
MORE PRODUCTS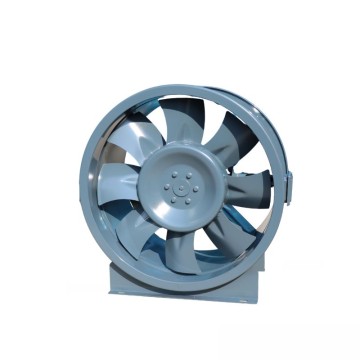
Combines advantages of axial and centrifugal fans, delivering high air pressure and large airflow for efficient ventilation in large commercial spaces.
MORE PRODUCTS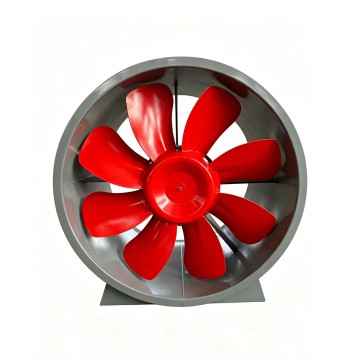
Specially built for fire smoke exhaust in buildings. Delivers strong air volume, high temperature resistance, and stable performance to quickly remove smoke.
MORE PRODUCTS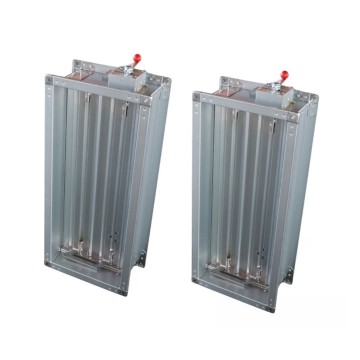
Built with heavy-duty galvanized steel, featuring reliable 70°C / 280°C temperature control, fast closing, and excellent fire resistance for HVAC ducts.
MORE PRODUCTS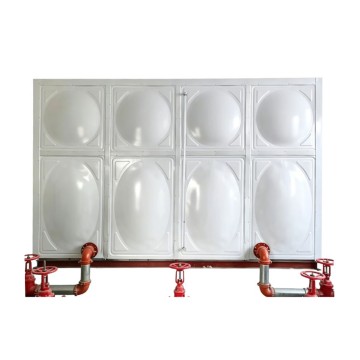
High-quality steel plate with high-temperature sintered enamel coating. Excellent corrosion resistance, smooth non-toxic interior meeting drinking water standards.
MORE PRODUCTS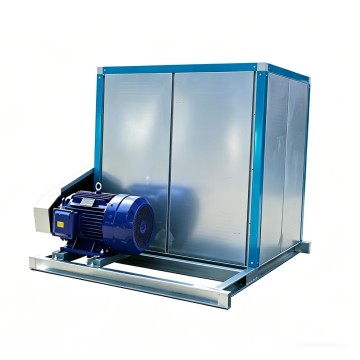
Integrates a high-performance motor with sound-insulated steel enclosure for efficient ventilation while reducing noise — ideal for indoor mall environments.
MORE PRODUCTS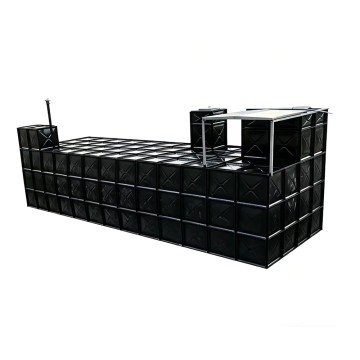
Specially designed for underground installation to save space and ensure stable fire-fighting water supply. Strong structural strength with excellent anti-corrosion performance.
MORE PRODUCTS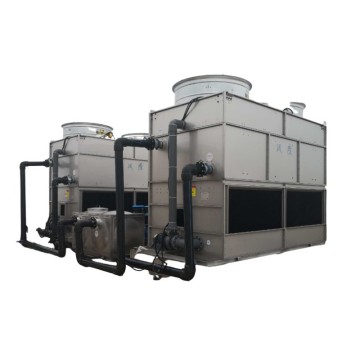
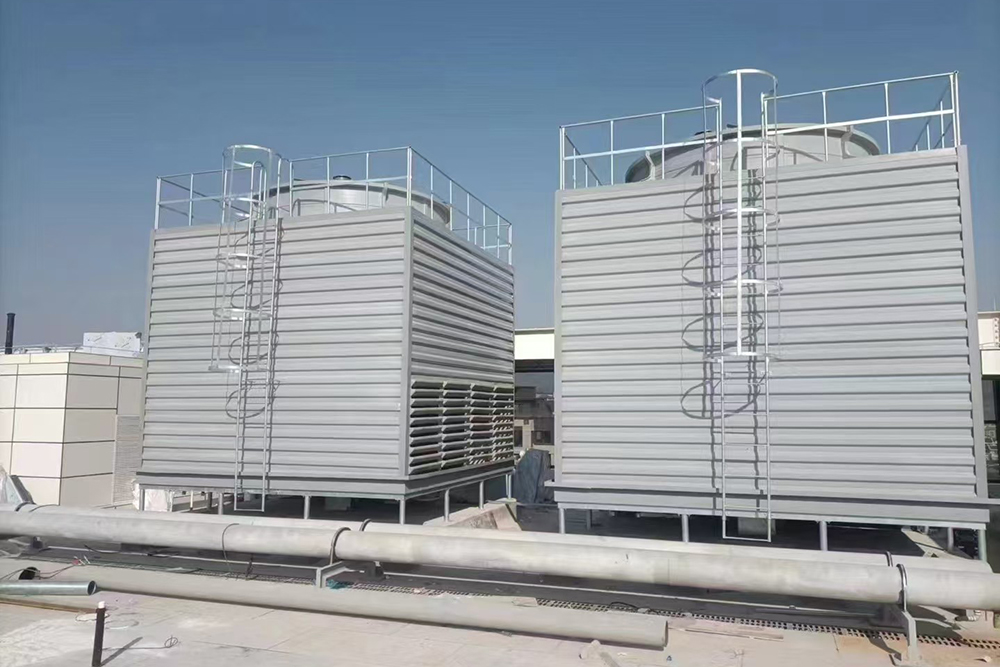
Fully enclosed coil system preventing circulating water from contacting air. Stable, high-efficiency heat dissipation ideal for large commercial HVAC applications.
MORE PRODUCTS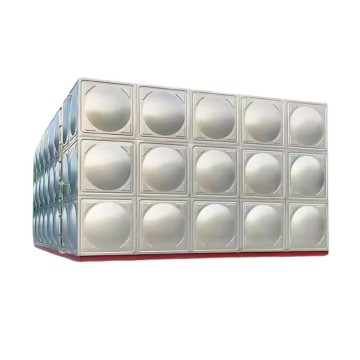
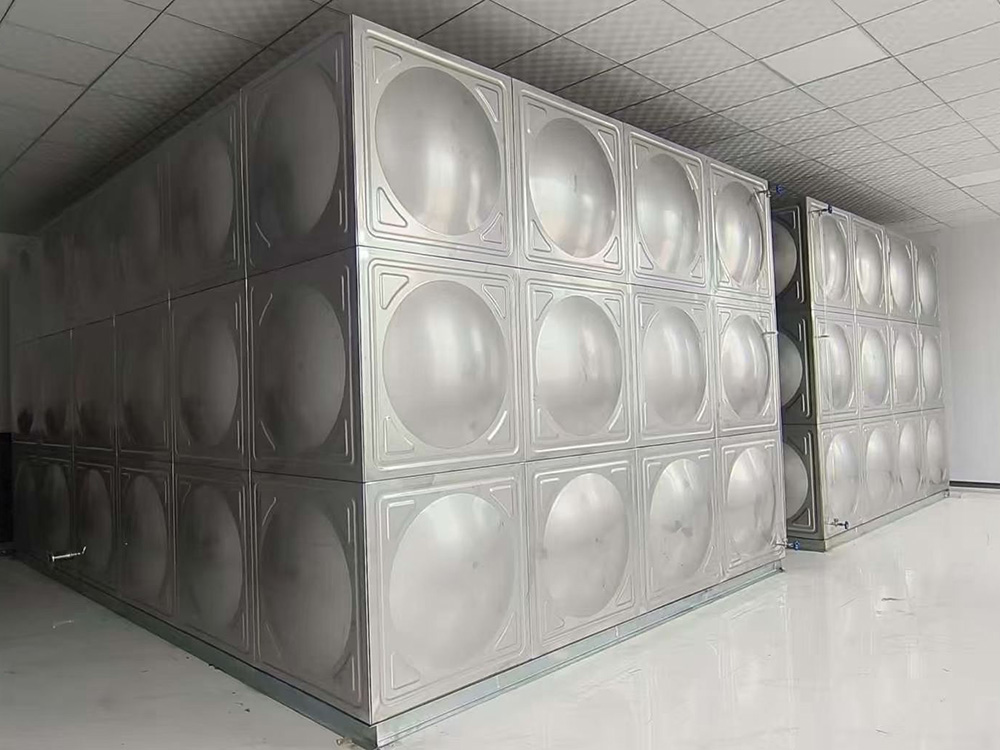
Crafted from high-quality SUS304/316 material ensuring food-grade safety, corrosion resistance, and long-term durability for commercial water applications.
MORE PRODUCTSGet factory-direct pricing on custom enamel steel water tanks engineered specifically for mega shopping malls, commercial plazas, and large-scale mixed-use developments. Our engineering team provides full-cycle support from design consultation to on-site commissioning.
GET A FREE QUOTE TODAY